
A centrifugal pump that runs dry for even a few seconds can incur damage such as scored seals and pitted impellers. On a small system, that’s an inconvenience. On a large-scale processing line, one pump often feeds an entire run of tanks or a full CIP loop. A pump priming failure there means downtime that ripples through the whole schedule.
Pump priming clears air from the suction line and casing so the pump can move liquid instead of drawing in air and cavitating. Smaller systems tolerate manual priming just fine: an operator opens a valve, watches for steady flow, and closes the valve again. A long suction run takes longer to purge, so an operator can’t always tell by eye when the line is actually clear.
A shifting tank level changes how long priming takes from one startup to the next, so there’s no fixed wait time to rely on. And a plant running multiple pumps has more lines needing that kind of attention than one operator can watch at once.
Pump Priming Breaks Down at Manual Scale
The math works against manual priming as systems grow. Every added pump is another point where a missed prime cycle can cause damage. Every added suction line means more length for air to travel through before flow starts. Large-scale processors across the cheese and dairy industry often run dozens of pumps across several production lines. That’s more than any crew can watch closely enough to catch every failed prime before it causes wear.
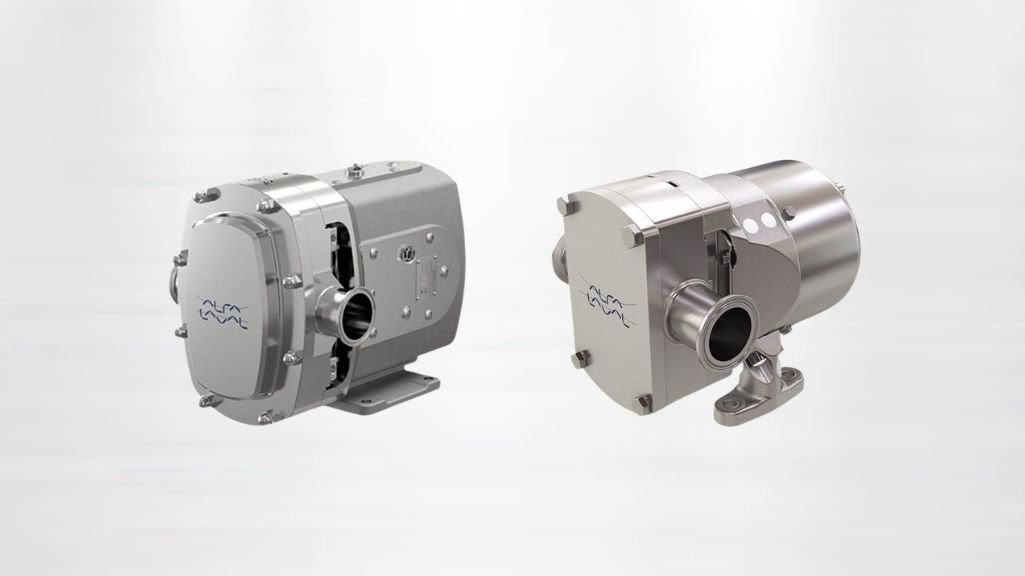
Dry running is the real cost here. Mechanical seals depend on the pumped fluid for lubrication and cooling. A pump that cycles without prime, even briefly, heats those seals past their rated tolerance. That shortens seal life in a way that’s hard to see day to day. The damage builds quietly until a seal fails at an inconvenient moment, usually mid-run.
What Automated Priming Systems Actually Do
Automated priming systems typically use a vacuum-assisted or self-priming design. They detect when a pump loses suction. Then they reestablish flow without anyone stepping in. Some rely on a dedicated vacuum pump tied to a discharge pressure sensor. Others use a self-priming impeller that recirculates liquid inside the casing until the air clears completely. Either way, the guesswork disappears from a process that used to depend on someone catching a problem in real time.
The same logic drives interest in automated tunnel washers that replaced manual washing hours on the sanitation side of a plant. Once a task like that gets automated, the labor it frees up goes toward higher-value work instead of babysitting equipment.
Sensor-based priming adds another layer. It tracks discharge pressure continuously. It flags a loss of prime before that turns into a dry-run event. That kind of monitoring turns priming from a one-time startup task into an ongoing check. That matters most on lines that start and stop often through a shift.
Maintenance Still Matters, Automation or Not
Automating the priming process doesn’t remove the need for a maintenance program behind it. The Hydraulic Institute’s maintenance checklist calls for gland packing checks, bearing lubrication, and vibration monitoring as baseline tasks. That holds regardless of which priming method a pump uses. Predictive tools like vibration analysis flag developing problems before they turn into failures. The Department of Energy’s maintenance guidance for pumping systems lays out this preventive and predictive split. The same logic applies whether priming is manual or automated: a documented maintenance schedule catches what daily operation alone won’t.
That same shift toward continuous monitoring is showing up elsewhere in dairy processing too. Sensor-based predictive maintenance programs now track equipment condition in real time instead of waiting for a scheduled inspection to catch a problem. Priming and predictive maintenance are really the same idea applied at different points in the pump’s life.
Pump Priming Built Into the Rest of the System
A priming failure on a line feeding an HTST pasteurizer can interrupt a thermal process mid-run, and that risk rarely stays contained to the pump itself. That usually means discarding product that never finished pasteurizing correctly. Catching a priming problem before it cascades costs far less than cleaning up after it does. That’s true whether the line runs milk, whey, or a cleaning solution through the same piping network.
Koss Industrial works with processors to specify pump and priming setups that match the scale of the system, not a one-size answer pulled from a catalog. Every line has its own suction length, tank geometry, and duty cycle. The setup should reflect that from the first drawing, not a catalog default. If a large-scale line needs automated priming built in rather than bolted on later, reach out to the Koss team.


