
High Temperature Short Time (HTST) pasteurization was built around fluid milk. Featuring predictable fat and protein content, this product moves through an HTST pasteurizer at a steady and familiar rate. However, many modern dairy products don’t always behave the same way. Protein-fortified milks, high-protein yogurts, and calcium- or vitamin-enriched formulas display different behavior when moving through the same equipment.
Liquids with higher protein and total solids content change how a product responds to heat. Proteins denature and interact differently at higher concentrations. Products with more body move through a heat exchanger differently than standard fluid milk does. Equipment tuned for conventional milk won’t automatically deliver the same result for high-protein formulas. This gap shows up in fouling rates and holding times. Occasionally, it also affects the finished product’s texture.
Why Higher Protein Content Changes the Thermal Math in an HTST Pasteurizer
Under the Pasteurized Milk Ordinance, products with more than 10 percent fat or 18 percent total solids already need higher pasteurization temperatures than the standard minimum. Denser products need more thermal energy to reach the same lethality all the way through. Functional dairy products with added protein isolates or concentrates often land in that higher-solids category.
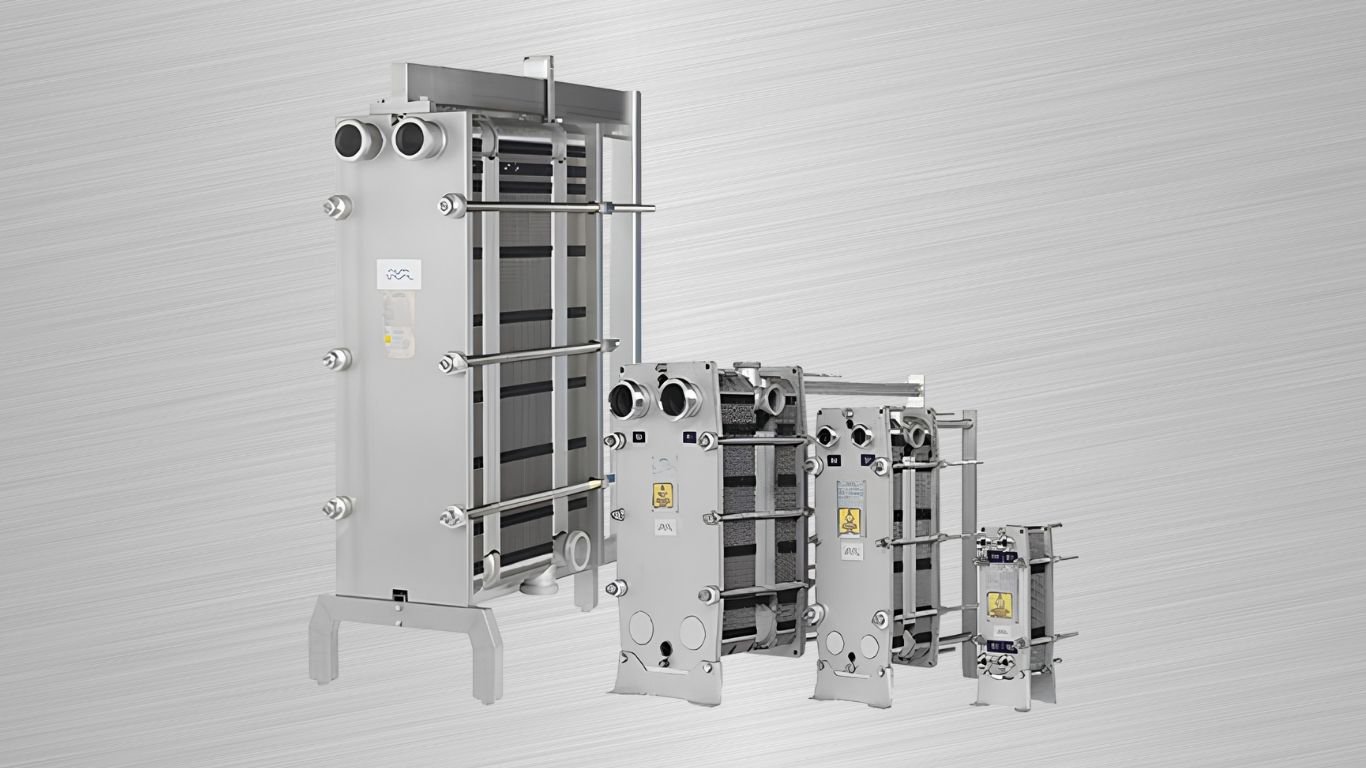
Higher-protein products also leave more residue on heat exchanger plates during runs compared to standard milk. That residue builds up over the course of a run and gradually reduces heat transfer efficiency. Eventually, this can affect the temperature the product actually reaches by the time it exits the holding tube.
Tracking that fouling curve in real time is one reason why predictive maintenance became standard in dairy lines. The system can flag efficiency loss before the problem reaches the product. A pasteurizer that runs clean for a full shift on standard milk may need a mid-run check much sooner on a high-protein formula. How often depends on how much residue that specific product leaves behind per pass, not a fixed schedule.
The HTST Pasteurizer’s Holding Tube Design Has to Account for Viscosity
The holding tube is where product sits at pasteurization temperature for the required time before cooling. It’s engineered around a specific flow profile that has to guarantee every particle of product gets the minimum holding time. Higher-viscosity products move through that tube with a flatter velocity profile across the tube’s cross-section. Liquid near the tube wall can end up under-processed if the tube size didn’t account for viscosity.
A plant needs to size holding tube length and diameter for the specific product’s viscosity, not assume standard milk flow traits apply. That’s what keeps a functional dairy line compliant without over-processing the product and hurting its texture or flavor. Skip this step, and a plant ends up choosing between two bad options. One is under-processed product near the tube wall. The other is a longer hold time that flattens flavor everywhere else.
Sizing the tube correctly is one of several factors worth checking against a new or used pasteurizer before assuming existing equipment can handle new formulations.
Functional Dairy Is Reshaping Equipment Investment
The shift toward these products isn’t a niche trend. A recent industry report from PMMI and FPSA, the 2026 Processing State of the Industry Report, names health-focused, protein-rich food production as a force reshaping equipment investment. Aside from HTST Pasteurizer upgrades, sanitation and automation demands are pushing in the same direction. Dairy already holds a solid share of processing machinery spending. Functional, protein-forward products are a growing part of that share, not a side note.
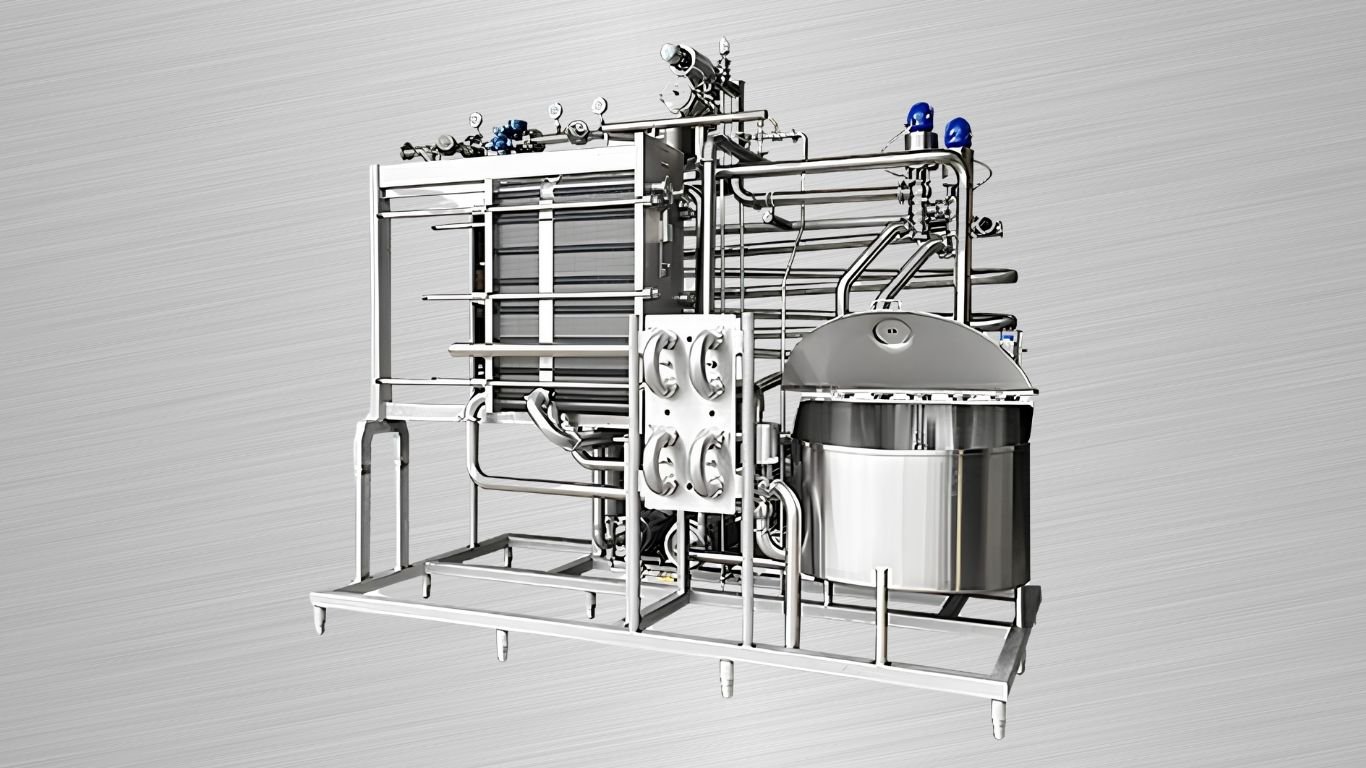
Processors adding a functional product to an existing plant often find their current pasteurizer wasn’t built for the new product’s fouling rate or holding tube needs. That mismatch doesn’t usually show up on paper. It shows up instead in a failed temperature log or a customer’s texture complaint.
Sourcing an HTST Pasteurizer for the Product You’re Running
Retrofitting or resizing equipment for a functional dairy product starts with understanding its specific thermal and flow behavior. Koss Industrial works through plate configuration, holding tube sizing, and cleaning frequency with processors across the dairy and beverage industries, bringing new functional products online. That work often runs alongside upgrades to tank cleaning equipment built for the same higher-fouling duty. It can mean retrofitting aging processing lines or searching out new equipment from the start.
A pasteurizer that ran fine on standard milk for years doesn’t automatically clear a high-protein reformulation. If a formulation change is coming, the Koss team can check whether the current HTST pasteurizer’s plate configuration and holding tube can actually handle it.


